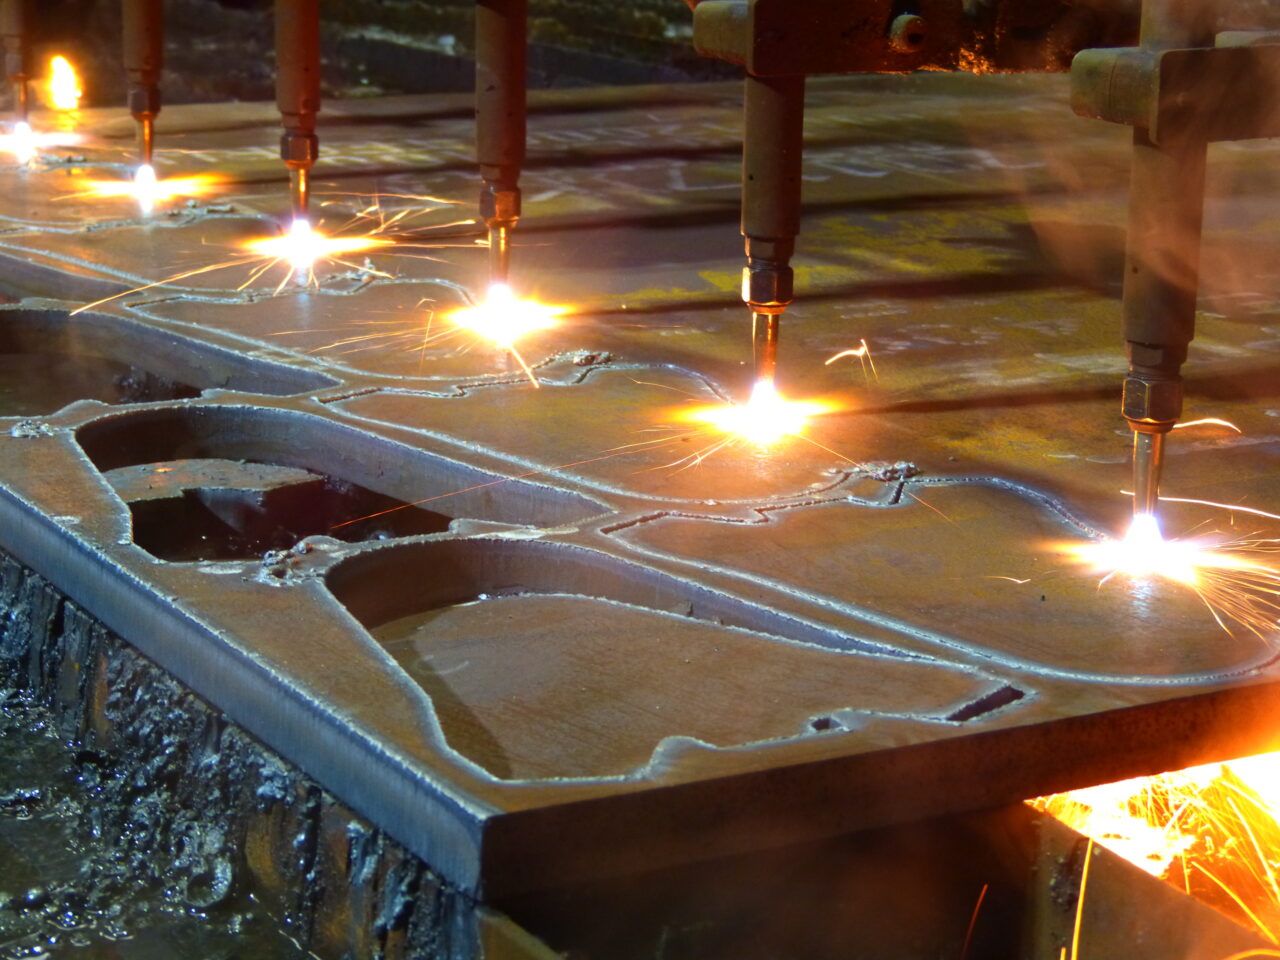
Oxy-fuel and plasma cutting of thick plate
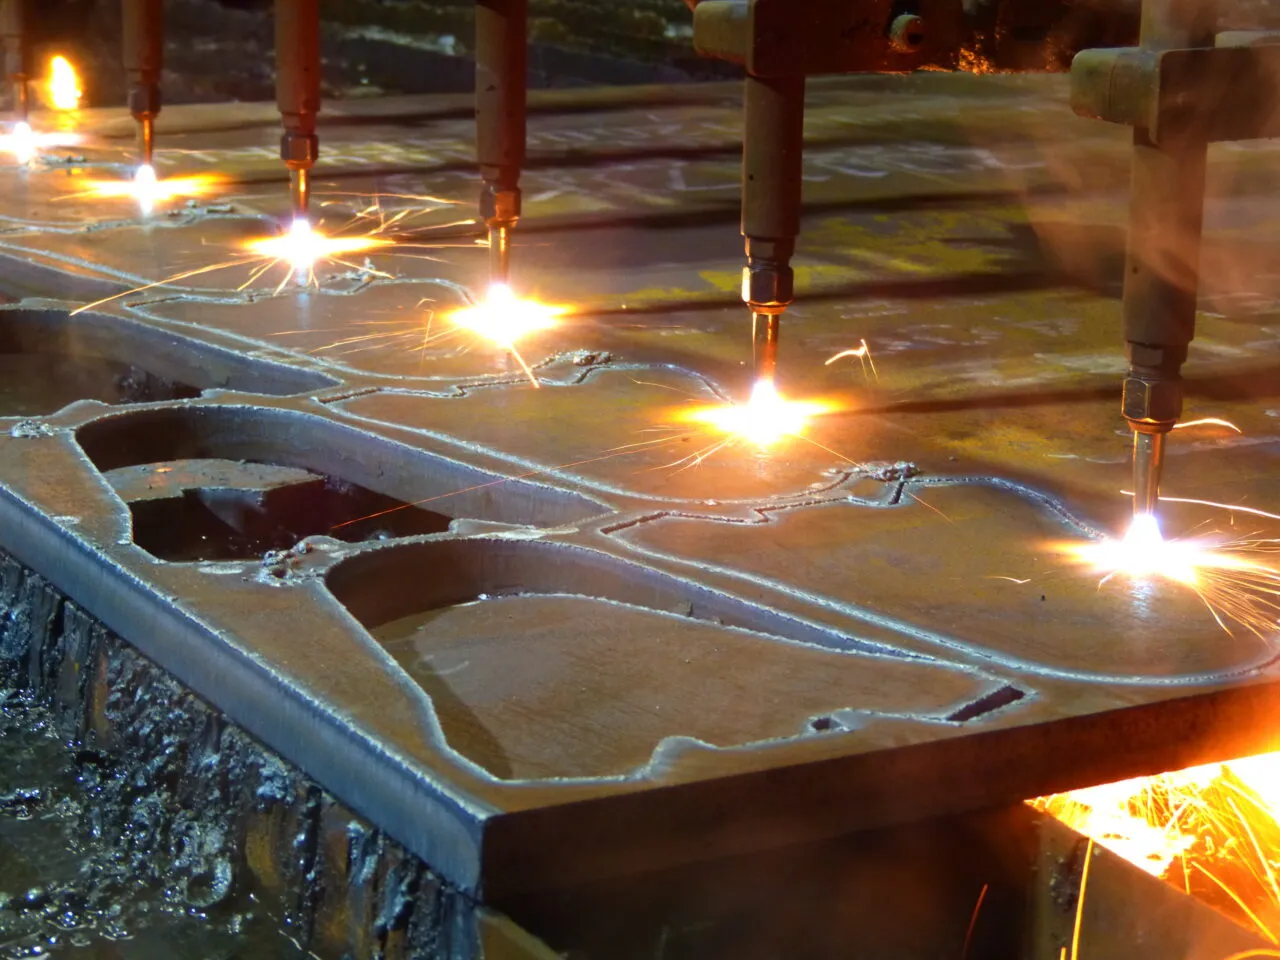
XXL Messer multi-torch table: oxy-fuel up to 300 mm, plasma up to 40 mm.
When plate is too thick for a laser, it goes on our XXL Messer cutting table. Several oxy-fuel torches cut at the same time, so a full plate of identical parts is cut in one pass; plasma takes medium thicknesses faster with a narrow heat-affected zone.
Oxy-fuel cuts carbon and low-alloy steel up to 300 mm thick. Plasma cuts up to 40 mm and leaves an edge that is ready for welding. Typical parts are counterweights, base plates, flanges, lifting lugs, brackets and structural gussets for heavy machines.
Thick parts usually need more than a cut: we flatten them in our straightening press, bevel the edges for full-penetration welds and shot blast them before shipping.
What it changes for you
- Feature
XXL Messer table with several oxy-fuel torches
BenefitA full plate of identical parts is cut in one pass, which keeps series lead times short.
- Feature
Oxy-fuel cutting of thick plate
BenefitCounterweights, base plates and flanges are cut in one piece from solid plate.
ProofCarbon and low-alloy steel up to 300 mm
- Feature
Plasma cutting
BenefitFaster than oxy-fuel on medium plate, with a narrow heat-affected zone and an edge ready for welding.
ProofUp to 40 mm
- Feature
Flattening and bevelling in the same plant
BenefitThick parts leave flat and weld-ready, without a second supplier.
Frequently asked questions
- Which grades can you oxy-cut?
- Carbon and low-alloy structural steels such as S235 and S355, and quenched and tempered high-strength plate. Stainless steel and aluminium are cut by laser or plasma instead.
- Can you cut weld bevels directly?
- Yes, bevels are made by gas or on our CNC bevelling machines, depending on the angle, land and thickness.
Have a drawing? Send it — an engineer answers.
STEP, DXF or PDF files are welcome.